Understanding the Role of Mineral Additives
Water treatment involves more than removing unwanted substances. Once purification takes place, carefully selected minerals can help restore desirable characteristics and support a balanced final composition. Food-grade mineral additives are formulated with attention to purity, consistency, and suitability for applications where treated water comes into contact with food or beverage processes. Their controlled composition makes them useful in systems that require dependable mineral supplementation without compromising quality. From processing facilities to specialised water treatment operations, mineral additives can serve a practical role in refining treated water characteristics. Proper selection also helps maintain process consistency, particularly where formulation and water quality must remain carefully controlled.
Mineral Support for RO-Treated Water
Reverse osmosis systems are highly effective at reducing dissolved substances, yet the resulting water may require selected minerals to achieve the desired composition for particular applications. This is where Food grade mineral additives for RO systems can provide a purposeful solution, supplying specific mineral components according to process requirements. Such additives are selected for their purity and compatibility with applications involving treated water. Consistent particle quality and controlled composition are especially valuable when dosing accuracy matters. Whether used during remineralisation or as part of a broader formulation process, suitable mineral additives can help create a controlled water profile while supporting dependable treatment practices and product quality.
Why Purity Matters in Food Applications
Mineral ingredients intended for food-related applications require careful consideration because purity directly influences suitability and consistency. Impurities or uncontrolled variations can affect processing conditions, formulation results, and the overall character of the finished product. Food-grade materials are therefore produced and handled with specifications that address composition and quality requirements. Clear product information can also assist technical teams in selecting an ingredient according to its intended application. For water treatment and food processing environments, dependable mineral quality supports repeatable results. Attention to sourcing, storage, handling, and dosage further contributes to a controlled process, particularly when minerals become an intentional part of the final formulation.
Potassium Bicarbonate for Controlled Mineral Formulation
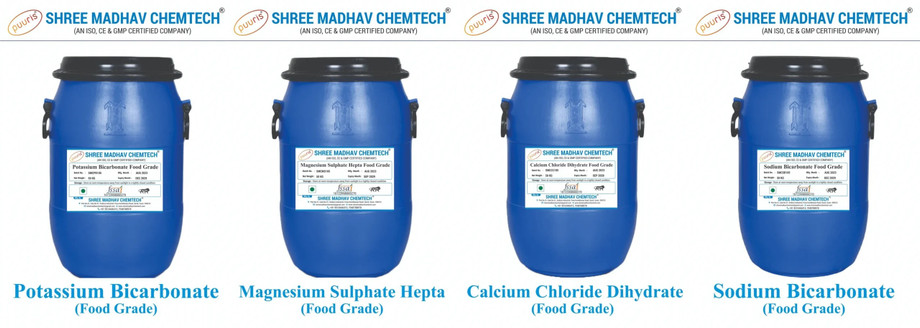
Among specialised mineral ingredients, Potassium bicarbonate food grade has applications where potassium and bicarbonate are required within a carefully managed formulation. Its chemical properties make it relevant to selected food, beverage, and water treatment processes where controlled mineral contribution is important. Product consistency is essential when incorporating potassium bicarbonate into established procedures, as variations can influence dosing and formulation outcomes. A suitable grade should therefore align with the intended application, handling conditions, and technical specifications. When used appropriately, potassium bicarbonate can contribute functional value while maintaining the ingredient standards expected in food-related environments. Precise measurement and proper storage remain important throughout its use.
Selecting Minerals for Specific Applications
Every treatment or formulation process has its own technical requirements, making mineral selection a matter of application rather than simple substitution. Factors such as required mineral concentration, solubility, purity, dosing method, and compatibility with existing equipment can influence the appropriate choice. Technical specifications should be reviewed carefully before introducing an additive into a process. Consistent quality is particularly valuable in commercial environments where repeated batches need predictable characteristics. Packaging and storage conditions also deserve attention because moisture and unsuitable handling can affect powdered mineral products. A considered approach to ingredient selection helps maintain process control and supports smooth integration into established water treatment or food production workflows.
Building Consistency Through Quality Ingredients
Reliable mineral supplementation begins with ingredients that meet clearly defined quality expectations. Food-grade mineral additives can support applications ranging from remineralisation processes to specialised food and beverage formulations when selected according to precise technical needs. Consistency in composition, particle characteristics, purity, and handling can make routine dosing easier and help maintain stable processing conditions. Clear documentation and suitable packaging further support responsible ingredient management. With the right mineral chosen for the intended purpose, treatment processes can be managed with greater precision and confidence. Careful specification, controlled dosing, and appropriate storage together create a practical foundation for maintaining quality across ongoing production and water treatment operations.